Quick answer
Control production color with a system, not a message saying “same as sample.” Define the approved physical reference, viewing light, comparison method, measurement locations, acceptable variation, lot identity and decision authority before bulk production. Review first-batch material before it is consumed, keep retained samples from every lot, and never mix shades inside a pair, set or retail unit unless the buyer has approved the result.
Who should use this guide
This guide is for overseas buyers developing private-label footwear, shoe soles, handbags, apparel or other products in which several materials must look consistent across samples, components and repeat orders.
Color risk is not limited to dyeing. Different material lots, coating thickness, molded-compound variation, texture, finishing, storage or viewing light can all affect appearance. A supplier can match one sample and still deliver inconsistent production.
The buyer’s task is to make the color decision reproducible. A different reviewer, on a different day, should be able to identify the controlling reference, use the agreed viewing condition and reach a defensible accept, hold or reject decision.
Start with a controlled color approval package
A screen image, phone photograph or color name is useful for communication but weak as the only production control. Displays, cameras, compression, white balance and ambient light can all change appearance.
Build an approval package with five connected parts:
- Physical master: the approved material swatch, component or finished sample, identified and protected from casual replacement.
- Digital record: clear photographs and an approval record that identify the reference, revision, supplier, material, finish and approval date without pretending the photograph is the color standard.
- Viewing condition: the agreed light source, viewing geometry, background and acclimatization or conditioning requirement where relevant.
- Comparison rule: locations to compare, permitted range, pair or set-matching requirement and who may approve a deviation.
- Lot traceability: a practical way to connect incoming material, components, work in process and packed goods to the lot that produced them.
The physical master can age, become dirty or be lost. Define its storage, handling and replacement process. When risk justifies it, keep synchronized buyer and supplier masters.
Define what “match” means for the product
One tolerance rarely controls an entire product. Texture, gloss and curvature affect perceived color even when the underlying colorant is similar. A smooth leather panel and a textured rubber outsole should not be judged as if they were flat pieces of the same material.
| Control question | Buyer decision to record | Useful evidence |
|---|---|---|
| Reference | Which physical sample, swatch or component controls the decision? | Reference ID, dated approval record and protected master |
| Viewing condition | Under which agreed light and background is the visual comparison made? | Viewing setup photograph and written instruction |
| Comparison locations | Which areas must be compared, and which areas are excluded because of edge, texture or process effects? | Marked diagram or controlled product image |
| Within-unit consistency | Must left/right shoes, front/back panels, lining pieces or hardware match each other? | Pair- or set-level comparison record |
| Across-unit consistency | How much visible variation is acceptable within one production lot? | Approved range or shade grouping |
| Across-batch consistency | Must repeat orders match the original master, the previous approved batch or a newly approved reference? | Batch approval history and retained samples |
| Decision authority | Who can accept, hold, regrade or approve a deviation? | Named approval workflow and written disposition |
If numeric color data is used, the buyer and supplier must agree on the instrument, settings, sample preparation, measurement locations and calculation method. A number without a controlled method can create false precision. Instrument readings may support the decision, but they do not automatically replace visual review of texture, gloss, pairing and end-use appearance.
Approve material before it disappears into production
The cheapest time to stop a color problem is before cutting, molding or assembly converts it into finished inventory.
For fabric or leather, review pieces from the actual lot before cutting. For molded soles or plastic components, review parts made with the intended compound, pigment, mold and surface. For coated hardware, compare production pieces—not only a finish chip.
Record the decision as released, held, conditionally released or rejected. “Looks okay” in a chat thread is difficult to trace later. A conditional release should state the exact limitation: for example, a defined shade may be used only within one order group and may not be mixed with another lot.
Build a shade map before cutting or assembly
When natural or process variation exists, group material or components into visually coherent shade bands before they are combined. The purpose is not to hide variation. It is to prevent an avoidable mismatch inside the customer’s field of view.
A practical shade-mapping workflow is:
- Confirm lot identities at receiving and keep unverified lots separated.
- Compare representative material under the approved viewing condition.
- Define temporary shade groups only within the buyer-approved range.
- Mark or route groups without writing on visible product surfaces.
- Cut or assemble matching components from the same approved group where the construction requires it.
- Recheck after finishing because heat, adhesive, polishing, coating or cleaning may shift the final appearance.
- Retain a dated sample from each released lot and link it to the order record.
This is especially important for footwear pairs, handbag panel sets, apparel body panels and products with mirrored components. A minor difference between separate units can become obvious when two mismatched pieces are placed side by side.
Inspect color at more than one gate
Color approval should not be a single event at final inspection. Use gates that reflect where the appearance can still change.
- Incoming gate: verify lot identity and material appearance before consumption.
- First-output gate: inspect the first acceptable pieces after molding, cutting, printing, coating or another color-sensitive process.
- Assembly gate: compare adjacent components after they are combined.
- Finishing gate: compare the final surface after polishing, washing, spraying, edge paint, buffing or cleaning.
- Packing gate: confirm that matched pairs or sets remain together and that mixed shade groups have not entered one carton assortment.
- Retained-sample gate: store a representative approved production sample for complaints, repeat orders and supplier comparison.
At each gate, define the unit checked, sample selection, reviewer, result and disposition. Do not use an inspection photograph as the only evidence of color; it is evidence that a comparison occurred, not a reliable substitute for the controlled physical comparison.
When production does not match
First contain the suspect lot. Identify which material lots, dates, lines, machines, finishing batches and packed goods may be affected. Do not blend held and released goods while the cause is being investigated.
Then separate four questions:
- Is the apparent difference caused by the viewing setup rather than the product?
- Is the variation inside one unit, between units in one lot, or between different lots?
- Did the supplier use the approved material, formula, finish and process route?
- Can the goods be sorted or reworked without creating another quality or compliance risk?
The written disposition may be release, regrade, sort, rework, replace or reject, depending on the approved specification. A supplier should not quietly use a different shade for replacement or repeat production. Any deviation needs a defined scope and written approval.
Boundaries buyers should keep clear
This framework does not set a universal color tolerance. Acceptable variation depends on the material, surface, product design, viewing condition, end use and buyer requirement. It also does not establish a laboratory standard or legal requirement.
Natural materials may vary in ways that cannot be managed like a flat synthetic surface. Metallic, pearlescent, fluorescent, translucent, textured and high-gloss finishes can change strongly with angle and light. For those products, agree on specialist methods and representative references before production.
Finally, do not “solve” a mismatch with uncontrolled reprocessing. Extra coating, heat, solvents, pigments or surface treatment can affect bonding, flexibility, odor, durability or compliance. Product-specific technical review should precede any recovery action.
The buyer’s pre-production color checklist
- Approved physical master is identified, protected and available at the supplier.
- Material, finish, color and product revisions are connected to the same approval.
- Viewing light, background and comparison locations are written down.
- Pair, set and across-batch matching rules are defined.
- Actual production material is reviewed before large-scale consumption.
- Lot identity remains traceable through cutting, molding, assembly and packing.
- Shade grouping and mixing rules are explicit.
- First output and post-finishing appearance are checked.
- Retained production samples are stored and linked to the order.
- Hold, deviation and release authority is named.
Next step
If color consistency is commercially important, send ZWC the product category, material and finish references, approved sample status, color-sensitive components, order quantity and supplier location. We can help structure the sourcing and production-control questions that need to be resolved before bulk release.
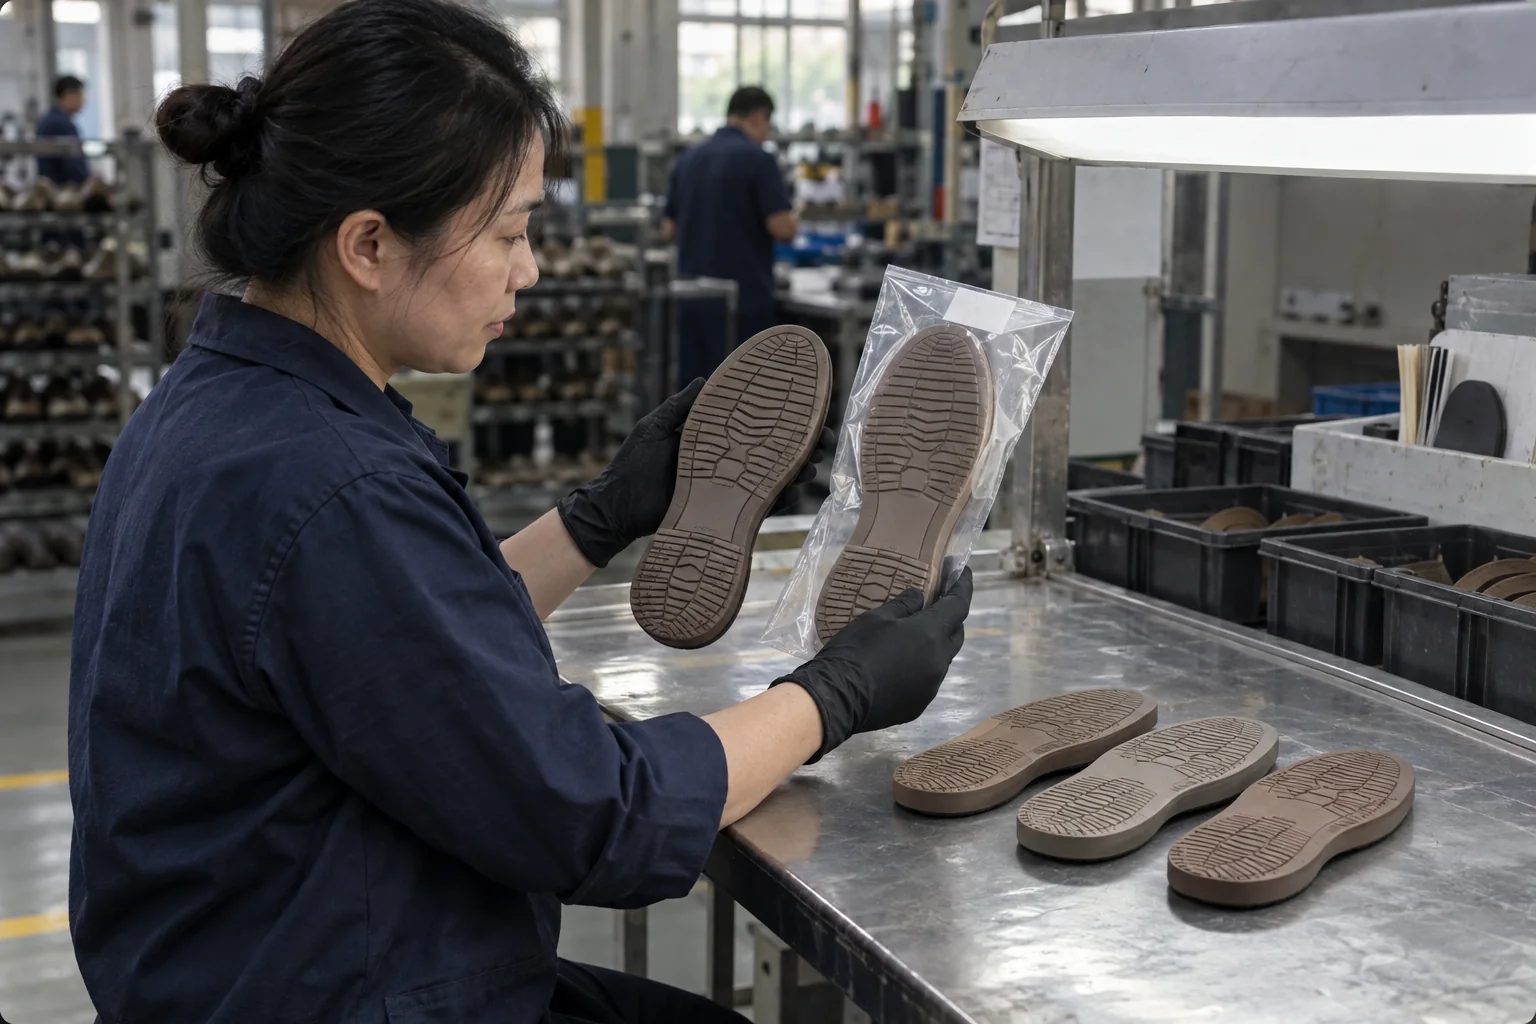
AI assisted with research organization, drafting and creation of the illustrative hero image. Buyer-specific technical, legal and commercial decisions still require verification for the actual product and order. The image is illustrative and does not depict a named ZWC client, supplier or verified project.