Quick answer
Do not accept “monthly capacity” as a standalone number. Verify the product route, available machines and people, working shifts, demonstrated cycle time, yield loss, changeover, planned downtime, committed orders and the slowest operation. Recalculate capacity for your exact style and order mix, then test the claim with a controlled pilot or early-production milestone before committing full volume.
Who should use this guide
This guide is for overseas buyers preparing a large first order, increasing volume with an existing supplier, or comparing factories that quote similar prices but very different lead times. It applies to private-label footwear, handbags, apparel, molded components and selected industrial products, although the actual bottleneck and evidence will differ by process.
Capacity verification asks whether the nominated site can complete the defined product mix, at the required quality level and within the agreed period, while honoring existing commitments.
Replace the headline number with a capacity model
A factory may quote output without defining assumptions. Request each input separately and distinguish supplier statements from buyer-verified evidence.
| Capacity input | What the buyer should define or verify | Useful evidence |
|---|---|---|
| Product route | Every major operation from incoming material to packed goods | Process-flow map tied to the quoted product |
| Working resources | Relevant machines, fixtures, lines and trained operators actually available | Dated site observations, equipment list and staffing plan |
| Working time | Shifts, hours, breaks, planned days and approved overtime assumptions | Production calendar and shift plan |
| Demonstrated rate | Output from a comparable product under normal conditions | Time study, line record or controlled trial |
| Yield and rework | First-pass output, normal loss, repair loop and scrap handling | Recent records for a relevant construction, with context |
| Changeover | Time lost between colors, sizes, materials, molds or styles | Changeover plan and sequence |
| Downtime | Maintenance, holidays, material delays and planned line stops | Maintenance calendar and production plan |
| Existing load | Confirmed orders already occupying the same constrained resources | Capacity-loading view with confidential details removed |
| Subcontracting | Which operations leave the nominated site and who controls them | Named process, approved location and control responsibility |
| Bottleneck | Operation with the lowest sustainable output for the required mix | Station-level rate and work-in-process observation |
| Packing release | Inspection, testing, rework closure and packing time after production | Shipment-readiness plan, not only ex-line date |
Show every assumption and unit. A monthly headline is not comparable with output per defined shift, construction and line.
Find the bottleneck before calculating output
Machine and headcount totals can look impressive while one specialized operation limits the order. Trace the actual product route around every constrained step.
For footwear, the bottleneck could be cutting, stitching, lasting, sole preparation, cementing, pressing, finishing or packing depending on the construction and factory. For handbags it may be skilled stitching, edge painting, hardware setting or repeated finishing. For apparel it may be a particular sewing operation, washing, printing, embroidery or final pressing.
Check whether the stated rate belongs to the bottleneck or a faster upstream station. Work-in-process accumulating before one operation is a useful signal, but compare the visit with recent records and the forward plan.
Use a transparent calculation
Build a simple scenario for each constrained operation:
Available production time × demonstrated good-output rate − planned losses = usable capacity
Keep the components visible. If the supplier gives only a gross cycle time, ask whether loading, unloading, inspection, changeover, breaks, maintenance, defects and rework are included. Do not apply an invented efficiency percentage to make the schedule look realistic; use observed or documented project-relevant inputs and label any remaining assumption.
Then compare usable capacity with:
- the buyer’s quantity by style, color and size;
- other confirmed orders using the same people, line, machine, mold or subcontractor;
- material arrival and approval dates;
- inspection, testing, correction and packing time; and
- the requested production-completion date.
A calculation that begins before materials and approvals are available is not a delivery plan.
Eight checks that expose weak capacity claims
1. Confirm the exact manufacturing site
Match the quotation and supplier identity to the place where the goods will be made. If part of production is subcontracted, record the process, location, approval route and responsibility for quality and timing. Capacity at an unrelated facility does not support the nominated order.
2. Walk the product route
Follow material movement from receiving through production, inspection, rework and packing. Note where batches wait, where tracking is lost, and which operations depend on scarce skills or shared equipment.
3. Compare three records
Request a forward plan, a recent record for a relevant product and the current work-in-process position. Confidential designs or prices need not be exposed, but dates, quantities, resources and status should form a coherent story.
4. Time a representative operation
Observe a normal run rather than a staged demonstration using the easiest size or best operator. Record product construction, number of people, machine or line, observation duration, good units completed and disruptions. A short observation provides an input, not proof of sustainable monthly output.
5. Test the style-mix assumption
One style in one color may flow differently from many colors, sizes or constructions. Ask how sequencing, mold changes, material lots, machine settings and packing assortments change usable time.
6. Inspect maintenance and spare constraints
Identify the critical equipment and tooling whose failure would stop the route. Review planned maintenance, repair responsibility and availability of essential spares or backup processes. A duplicate machine is not a backup if it lacks the necessary fixture, program or trained operator.
7. Separate overtime from base capacity
Treat overtime as a controlled contingency, not invisible base capacity. Confirm that working-time assumptions are lawful, safe, commercially accepted and consistent with buyer requirements. Do not use capacity pressure to justify unsafe work or unapproved subcontracting.
8. Verify through a milestone
Before relying on full-volume output, use a pilot, first-off approval or early-production checkpoint appropriate to the order. Compare planned versus actual start, good output, defects, rework, work-in-process and recovery actions. The result should update the delivery forecast rather than remain a ceremonial report.
A buyer-side capacity evidence pack
- controlled product and process-flow reference;
- site and resource list relevant to the order;
- shift and production calendar with assumptions;
- bottleneck-rate evidence and observation notes;
- yield, rework and changeover inputs with their source;
- material-readiness and tooling status;
- current loading of constrained resources;
- subcontracting map and control owner;
- milestone plan with responsible people and dates; and
- update cadence for output, defects, rework and shipment readiness.
The evidence pack should be proportionate to the commercial risk. A small repeat order does not need the same investigation as a new tool, a seasonal launch or a volume increase that occupies a major share of one line.
Red flags that justify a pause
- the factory repeats one monthly number but cannot show its assumptions;
- quoted capacity includes machines, people or sites not assigned to the order;
- the supplier cannot identify the likely bottleneck for the product route;
- lead time begins before material, tooling or sample approval can realistically be ready;
- the plan assumes perfect yield or hides rework outside the schedule;
- work already committed to the constrained line is not considered;
- subcontracting appears only after the order is placed;
- a brief staged run is presented as proof of sustained output; or
- the recovery plan depends entirely on overtime without safety and compliance review.
What capacity verification cannot prove
A capacity review cannot guarantee delivery, product conformity, worker availability, material arrival or uninterrupted equipment performance. It also cannot establish legal compliance, financial stability or long-term management capability by itself. Those questions may require supplier verification, audit, testing, contract controls, production follow-up and qualified advice.
Capacity is a forecast supported by evidence. Its value comes from exposing assumptions, identifying the bottleneck and updating the plan when actual output differs.
Prepare a capacity verification brief
ZWC Sourcing can help buyers organize the product route, supplier capacity inputs, bottleneck evidence and production milestones before a large order or volume increase. Send the product category, specification status, quantity and assortment, nominated site, target completion date and current supplier plan.
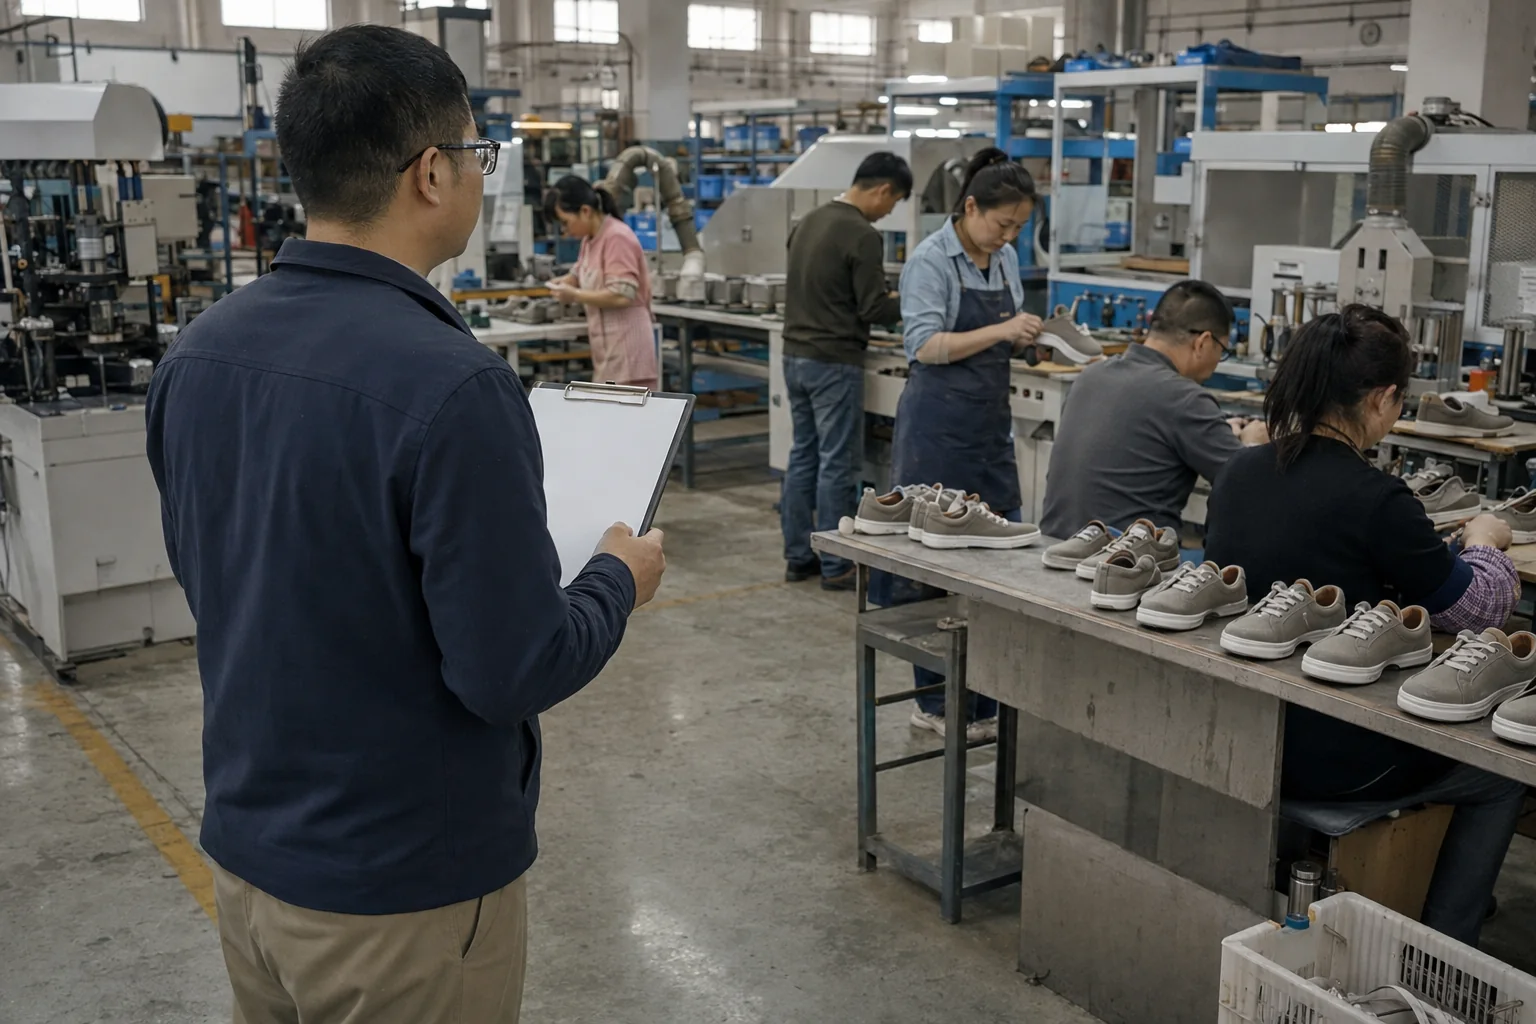
AI assisted with research organization, drafting and creation of the illustrative hero image. Buyer-specific technical, legal and commercial decisions still require verification for the actual product and order. The image is illustrative and does not depict a named ZWC client, supplier or verified project.